Maintenance
Daily, weekly and yearly maintenance for vacuum tube lifters
Compiled from public standards and manufacturers' published data.
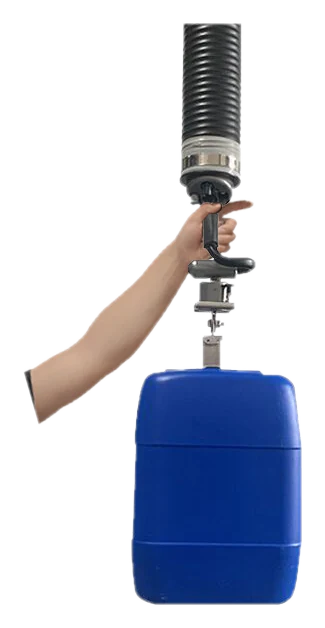
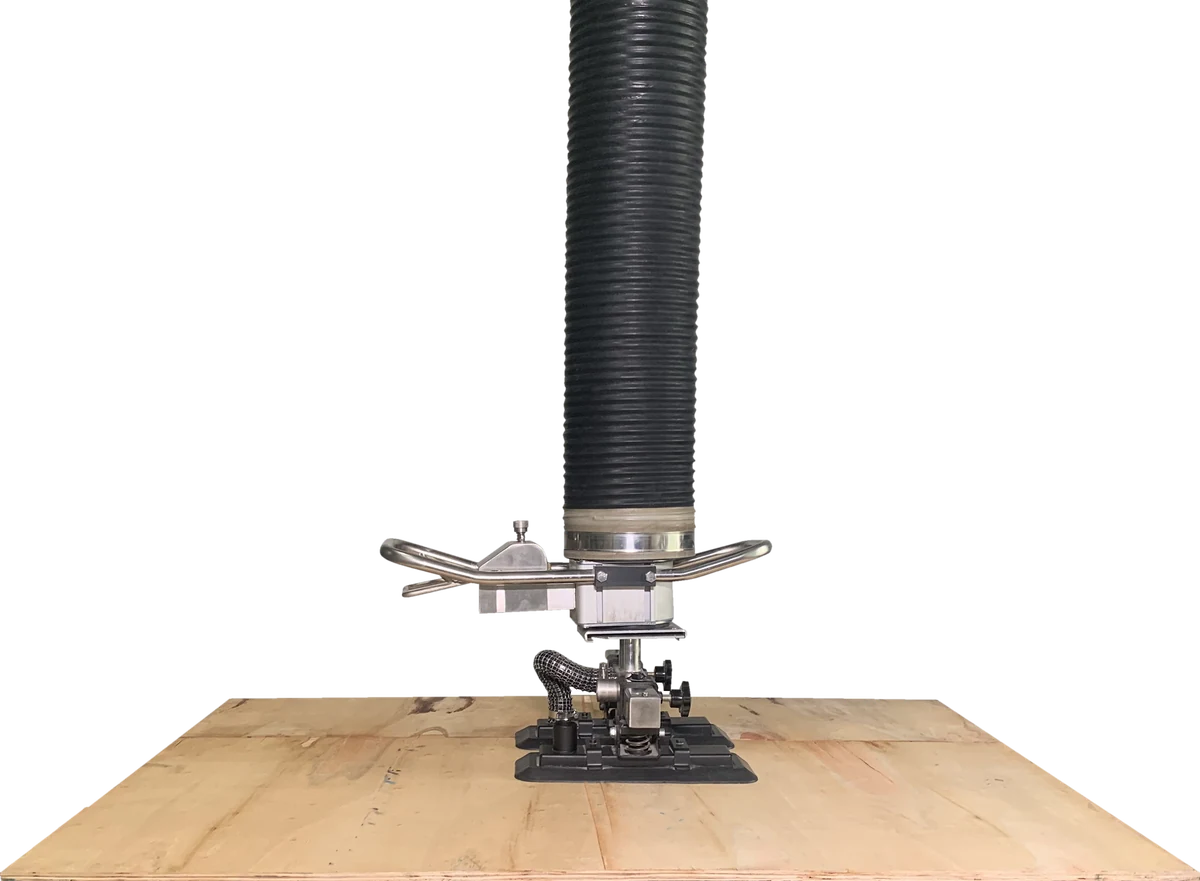
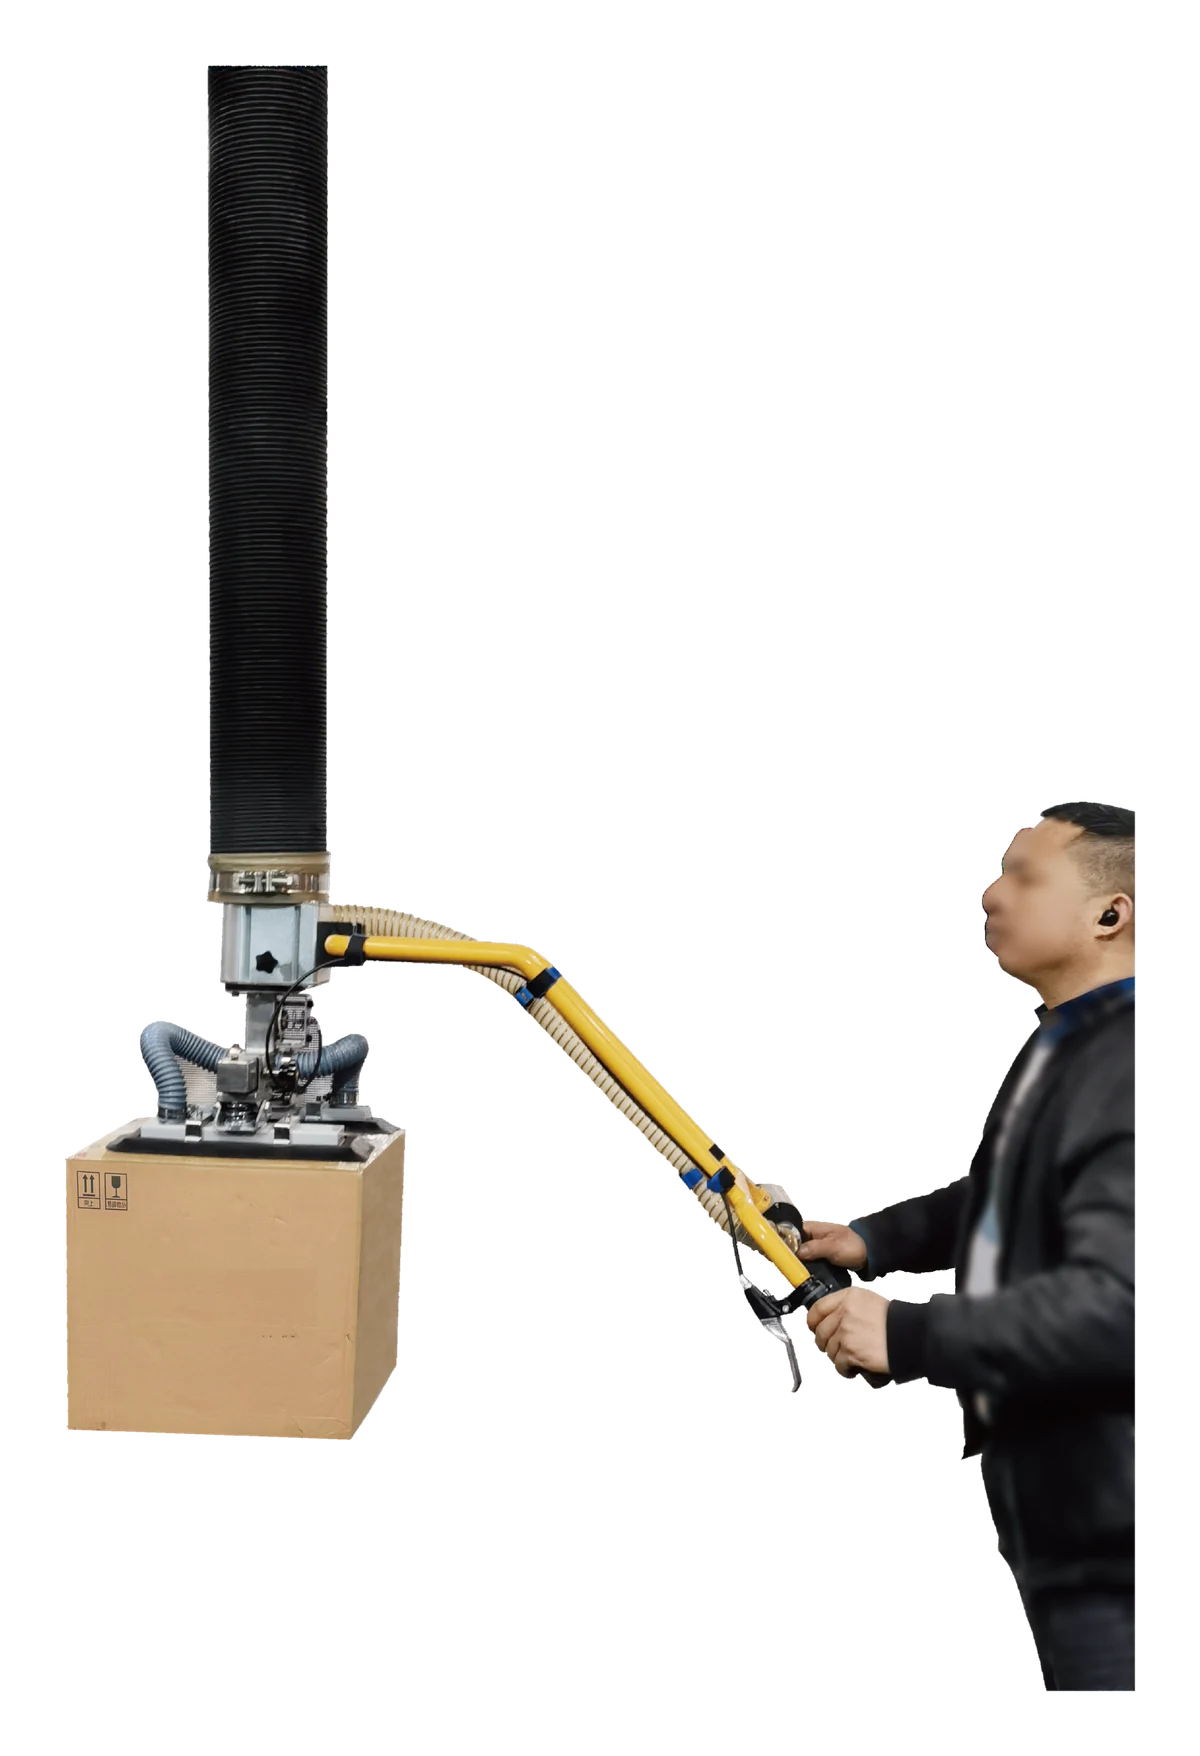
A vacuum tube lifter has few moving parts and a short list of things that wear: the pad seal, the lifting tube, the filters, the hoses and the valves. This vacuum lifter maintenance checklist collects what the industry checks before each shift, each week, each quarter and each year, the wear parts and their typical intervals, a troubleshooting table for lost capacity and slow lifting, and a note on statutory inspections. The intervals are industry practice; the manual of your model and your local rules take precedence. It applies to vacuum tube lifters in general, including our vacuum tube lifter range; the manual of your model takes precedence.
Daily pre-use checklist
Twelve checks before the first lift of the shift help find wear early. The daily check of the pad and the alarm devices follows the UK HSE guidance on vacuum lifting equipment, and the pre-use check of the load surface, controls, gauges and pump follows the practice of the US ASME B30.20 standard for vacuum lifting devices.
| # | Check | OK when |
|---|---|---|
| 1 | Inspection and service date still valid | Not expired |
| 2 | Lifting tube and wear cover: no cuts, bulges or wear-through | No damage |
| 3 | Hoses and clamps tight, no hissing | No leaks |
| 4 | Pad seal intact and clean | Intact, no debris |
| 5 | Pad or quick-change coupling locked; where colour-coded, codes match | Locked, matched |
| 6 | Filter not visibly clogged; clogging indicator normal, where fitted | Normal |
| 7 | Handle lifts, lowers, holds and releases smoothly | Smooth control |
| 8 | One test cycle with a typical load: grip, lift, hold, lower, release | All steps normal |
| 9 | Crane or rail moves freely, no unusual noise | Smooth |
| 10 | Capacity and warning labels legible | Legible |
| 11 | Vacuum gauge or indicator normal, where fitted | Normal |
| 12 | Nobody under the load; loads carried low | Complied |
A lifter that fails any check is taken out of use until the fault is corrected; damage to the lifting tube in particular means stop and replace, not patch. The HSE guidance suggests keeping the load low during travel, ideally below 1.5 m.
Next step: the wear parts behind the tube, hose, seal and filter checks are listed with order details on the spare parts page.
Weekly, quarterly, yearly
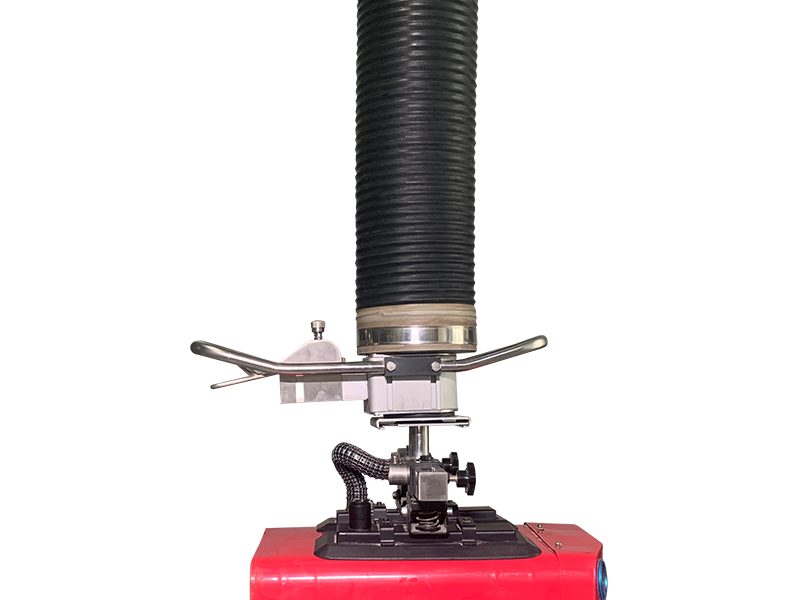
Beyond the daily check, the schedule used by manufacturers in this industry has three levels: the operator every week, in-house maintenance every quarter, an authorised service every year. The weekly list below is the common one; your model's manual sets the exact items and torques.
| When, by whom | Items |
|---|---|
| Weekly, operator | Yearly service date still valid; bolts and nuts undamaged; power-off safety test, described below; all connections: tube clamps at both ends, trolley hanger pin, hose clamps, pad bolts; pump-side and pad filters cleaned, more often in dust; lifting tube and hoses undamaged, replaced at once if not; capacity and warning labels legible; smooth travel on the rail or arm; operating valve working; the lifter still reaches its rated capacity, since a drop means a leak |
| Quarterly, in-house maintenance | Repeat the weekly items; check the crane or rail for damage, wear and loose bolts and pins |
| Yearly, authorised service | Full inspection to the manufacturer's yearly report, with the record updated; one manufacturer's manual notes that some countries also require a third-party inspection after installation and every year |
| Pillar jib crane, in addition | One US crane maker's manual: anchor bolts and arm connections every 500 hours or 3 months; rollers, arm level and a visual check every 1,000 hours or 6 months |
Switch off and isolate the power before any maintenance or repair. On lifters of this type, a common weekly power-off test is to lift a dense load of about the rated capacity, a steel plate for example, to about 1 m, close the handle and switch the pump off; on such lifters the load typically sinks slowly under control. Follow the test and the pass criterion in your model's manual; if the load does not behave as the manual describes, take the lifter out of use and call the supplier. After installation, all bolts are re-tightened within the first 1 to 2 months.
Wear parts and replacement intervals
The intervals below are industry experience and move with dust, duty and the load.
| Part | Check | Typical replacement |
|---|---|---|
| Pump-side filter cartridge and pad filter mesh | Weekly; blow out at low pressure | When it no longer cleans or is damaged; about 3–6 months in dusty plants |
| Pad seal lip, gasket or foam | Every shift, by eye | When worn, cut, hardened or shiny; about 3–12 months on sack duty; one maker of vacuum lifting devices advises at least every 2 years |
| Lifting tube | Every shift by eye, weekly in detail | At once when punctured, abraded, twisted or over-stretched; normally about 1–3 years |
| Tube wear cover | Weekly | When worn through |
| Hoses and clamps | Weekly | When cracked or loose; new clamps whenever the tube is refitted |
| Handle valve seals; top swivel and safety valve | Weekly function test | Valve seals at the yearly service as needed; a swivel or safety valve that fails its test means stop and repair by authorised staff |
Next step: part names, the kit we suggest ordering with the lifter, and how to order by model and serial number are on the spare parts page.
Troubleshooting
The most common fault is lost capacity, and it is mostly caused by a leak, a clogged filter, a damaged seal or an overload. Work through the table from the cheapest cause; anything that involves the lifting tube or the safety valve means stop first.
| Symptom | Likely causes | What to do |
|---|---|---|
| Load will not lift, or capacity has dropped | Pump not running or running backwards; overload; leak at a hose, clamp or the tube; clogged pump-side or pad filter; pad fitted crooked or with the wrong bolt torque; damaged pad seal; speed-control valve on the filter left open | Check pump and supply; reduce the load to the rating; find the leak section by section, tighten or replace; clean or replace filters; have an electrician swap the phases if the silencer blows the wrong way; refit the pad; replace the seal; close the valve |
| Load sinks slowly, will not hold | A small leak; a porous load; worn handle-valve seal; balance set wrong | Find and fix the leak; use a pad suited to the load or reduce the load; repair the valve; reset the balance. On lifters of this type, a controlled descent when the power is off is normally the safety function working, not a fault; your manual describes how your model behaves |
| Slow response, slow lifting | Clogged filter; hoses too long or kinked, more than 30 m in total; speed-control valve open; pump too small for the duty; low voltage or a missing phase | Clean the filter; shorten and straighten the hoses; close the valve; review the pump size; check the supply |
| Handle sits too high or too low | Balance set wrong | Reset the balance: with load first, then without |
| Pump will not start | Motor circuit breaker tripped; main switch off; thermal protection tripped; remote control flat or out of range | Find the cause, then reset; switch on; let it cool and check the ventilation; replace the battery or move closer |
| Noise, overheating | Load held suspended for long periods; poor ventilation; clogged filter; long or kinked hoses; no sound enclosure; frequent starts | Shorten hold times; keep the ventilation gap; clean the filter; sort the hoses; fit an enclosure; wait at least 60 s before restarting |
| Lifting tube damaged | Sharp edges; twisted wire; over-stretch; ageing; a clamp sitting on the wire | Stop and replace; fit a wear cover; never shorten or patch the tube without the manufacturer's approval |
| Filter clogs quickly | Burst or dusty sacks; pad filter mesh missing | Clean more often; fit the pad mesh; consider a larger pre-filter |
| Porous sacks will not hold, heavy leak | Wrong pad for sacks; load rated on an airtight load; woven or creased sacks; worn seal | Fit a sack pad; re-rate on the porous load; larger pad or vacuum source; replace the seal |
| Load sticks to the pad on release | Handle not pressed fully; release valve missing or wrongly fitted | Press the handle fully to break the vacuum; fit the release valve as the manual shows and use it only once the load is down |
| Lifter drifts along the arm or rail by itself | Arm or rail not level | Re-level |
Next step: if the table does not clear the fault, send us the model and serial number, a short video of the symptom and a photo of the filter and the seal through the enquiry form, and ask for the parts or the repair steps.
Statutory inspections
Maintenance and inspection both sit with the employer. In the EU and the UK, lifting equipment must be examined by a competent person after installation and at intervals; the interval and who counts as competent are set nationally, and other markets have their own rules. In the EU, the work equipment directive requires equipment whose safety depends on its installation to be inspected after installation, before first use and after reassembly at a new site, with periodic inspections for equipment that deteriorates, by persons competent under national law, with the results recorded; the frequency is set by each member state. In the UK, LOLER requires a thorough examination at least every 6 months for lifting accessories and at least every 12 months for other lifting equipment, or to a written scheme drawn up by a competent person, and the HSE guidance adds daily and weekly checks for vacuum lifting equipment. In the US, the ASME B30.20 standard describes three levels of inspection for vacuum lifting devices, each use, frequent and periodic, with intervals by service conditions; ask your inspector whether it is applied to tube lifters at your site. Rules as of September 2026; check the current text before relying on them.
Buying a vacuum tube lifter does not make a workstation compliant: the employer still carries out the risk assessment, trains the operators and has the equipment inspected as local rules require. HSE guidance treats a vacuum lifter that is moved between cranes as a lifting accessory, examined every 6 months, and one fixed to its crane as examined every 12 months or to the examination scheme; ask your competent person how this applies to your lifter.
Download the checklist
The daily and weekly checklists on this page are available as a one-page PDF to print for the workstation; it carries the same industry items as the tables above and no model-specific values.
To ask for a recommended spare-parts list for your model, use the form and state the model and serial number.
state the model and serial number.
Scope
What this page does not cover
Repair instructions for a specific model, which are in its manual; maintenance of other makers' lifters; and any shortening, patching or modification of the lifting tube, which needs the manufacturer's approval. The intervals on this page are industry practice; warranty terms, including any maintenance conditions, are confirmed in the quotation.
Cowest Machinery designs and manufactures vacuum tube lifters at its factory in Qingyuan, Guangdong, China.